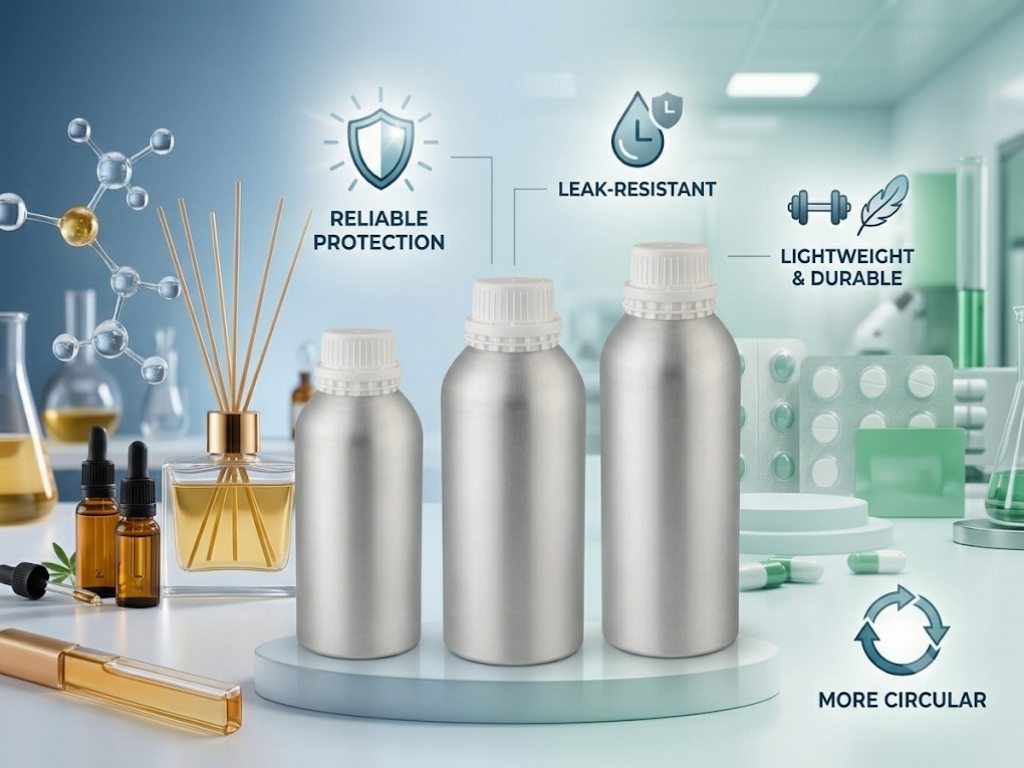
Packaging performance matters significantly in the fragrance and pharmaceutical industries, where leakage, product compatibility, transportation damage and exposure to external conditions can affect product quality and operational costs. This is why plugless aluminium bottles are gaining attention as a practical packaging format for sensitive and high-value products.
1. Reliable Product Protection
Aluminium provides an effective barrier against light and external environmental exposure. This can be particularly valuable for products that require controlled storage conditions. For pharmaceutical applications, however, the suitability of an aluminium canister or container depends on the formulation, closure system and any required internal coating.
For fragrance, essential oil and pharmaceutical manufacturers, selecting packaging with the appropriate barrier and compatibility characteristics can help maintain product integrity throughout storage and distribution.
2. Secure, Leak-Resistant Packaging
Leakage can mean product loss, damaged secondary packaging and additional handling costs. Plugless aluminium bottles are engineered for secure containment and can provide a practical solution where leak resistance is an important packaging requirement.
Their construction also offers good resistance to handling and impact during transportation compared with more fragile packaging materials.
3. Lightweight and Durable for B2B Supply Chains
For manufacturers and distributors, packaging weight affects handling, warehousing and transportation. Aluminium offers a useful combination of low weight and mechanical durability, helping businesses balance packaging performance with logistics requirements.
This makes aluminium bottles relevant for applications where products may pass through multiple stages of storage and distribution before reaching the end user.
4. Flexible for Fragrance and Pharmaceutical Applications
Fragrance and pharmaceutical products have different packaging requirements, so a standardised approach does not work for every formulation.
Aluminium bottles for fragrance, and aluminium canisters or containers for pharmaceuticals, can be supplied in different sizes, finishes and configurations, while internal coatings can be considered where product compatibility requires additional protection. Al-Can provides aluminium packaging solutions for applications including fragrances, flavours, essential oils and pharmaceuticals, subject to application-specific requirements.
5. A More Circular Packaging Option
Sustainability is increasingly becoming part of B2B packaging procurement. Aluminium is highly recyclable and can be recycled repeatedly without losing its fundamental material properties.
For brands looking to reduce packaging impact while maintaining durability and product protection, aluminium can therefore offer a strong balance between performance and recyclability.
Conclusion
The growing interest in plugless aluminium bottles reflects a broader need for packaging that combines secure containment, product protection, durability and efficient handling. For fragrance and pharmaceutical manufacturers, the right aluminium packaging format can support product integrity while meeting practical supply chain requirements.
With experience in aluminium packaging for specialised industrial applications, Al-Can offers solutions that can be evaluated according to product compatibility, packaging specifications and application requirements.
FAQs
What are plugless aluminium bottles?
Plugless aluminium bottles are aluminium containers designed without a separate conventional plug and engineered for secure containment through their specific bottle-and-closure configuration.
Are plugless aluminium bottles suitable for fragrances?
Yes. They can be suitable for fragrances, essential oils and related products, provided the aluminium, internal coating and closure system are compatible with the specific formulation.
Can aluminium canisters or containers be used for pharmaceutical products?
Yes. Aluminium canisters and containers can be used for pharmaceutical applications. However, selection should consider formulation compatibility, internal coating, closure performance and applicable regulatory requirements.
What are the main advantages of aluminium bottles?
Key advantages include lightweight construction, mechanical durability, protection from light and recyclability. The exact performance depends on the bottle design and application.
Why should businesses consider aluminium packaging?
For B2B manufacturers, aluminium can provide a combination of product protection, handling durability, transportation efficiency and recyclability, making it a practical option for demanding packaging applications.
This article is for general information only and is not technical, regulatory or professional advice. Please verify independently and consult qualified experts before making packaging decisions. See our full Disclaimer.

 info@alcanexports.com