Aluminium Canisters for Chemicals
Chemical products can have very different packaging needs depending on their formulation, concentration, storage conditions and transportation requirements.
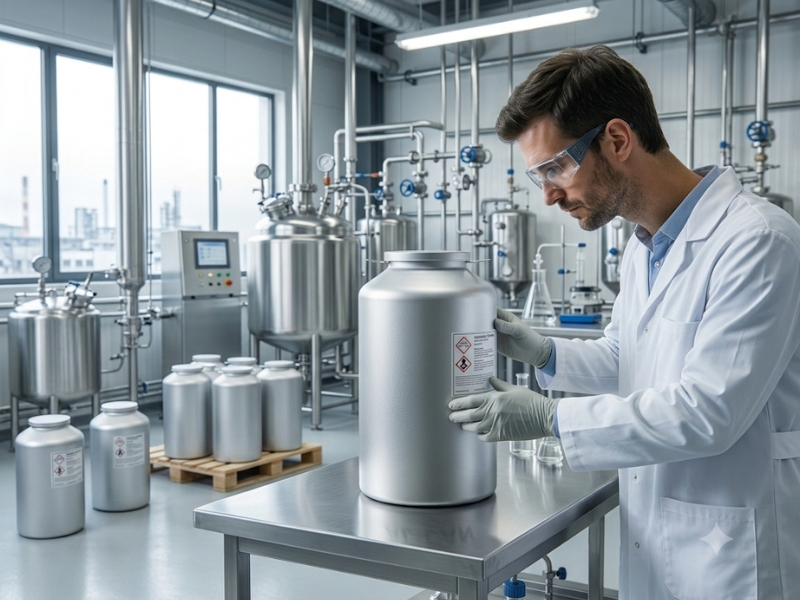
Al-Can manufactures aluminium canisters and containers for chemical, solvent and specialty industrial applications, with configurations selected according to the product and its handling requirements.
Request a Quote →
Applications
- Specialty chemicals
- Industrial liquids
- Sensitive formulations
- Solvents
- Chemical intermediates
- Laboratory and industrial chemicals
Why Consider Aluminium Canisters?
Durability
Aluminium canisters are robust enough for handling, storage and transportation.
Light Protection
Opaque aluminium helps limit exposure to light.
Coating Options
Internal coatings can be considered when required, subject to product compatibility.
Multiple Capacities
Choose from different canister and container sizes based on application needs.
Chemical Compatibility Matters
Container materials and coatings are not universally compatible with every chemical. The right configuration should be selected based on the specific formulation and the conditions in which the product will be stored and transported. Al-Can can review the application requirements with you before determining a suitable packaging configuration.
Need aluminium canisters or containers for chemicals?
Request a Quote →
 info@alcanexports.com